WESTERN MECHANICAL, INC. | Primary Dispatch: (661) 251-0111 | 24/7 Hotline: (800) 585-5085 | CSLB #618138 (C-20, C-38, C-4) | 100% UA Local 250 Union
Extending Galvanized Cooling Tower Cold-Water Basins 15 Years With Polyurethane Coating
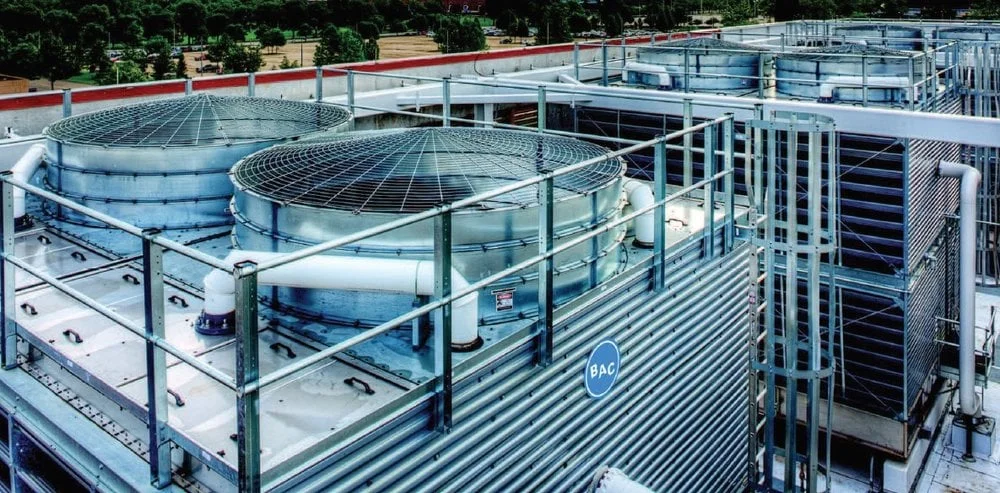
Specialized Abrasive Prep, Seam Reinforcement, and 40-80 mil Flexible Elastomeric/Epoxy Linings for Corroded BAC, Marley & Evapco Basins
Direct Engineering Summary
Western Mechanical, Inc. extends the service life of galvanized cooling tower cold-water basins by 15 years or more through specialized polyurethane and elastomeric epoxy coating applications. This process involves abrasive blasting to NACE 2/SSPC-SP10 near-white metal, seam reinforcement, and applying 40-80 mil thick flexible coatings. This method is highly effective for corroded BAC, Marley, and Evapco basins, often saving facilities over $250,000 compared to crane replacement costs. Our UA Local 250 journeymen ensure compliance with industry standards. Contact Western Mechanical, Inc., CSLB #618138, at (661) 251-0111 for expert service.
Engineering Tolerances & Governing Standards
Parameter
Specification
Standard
Coating Thickness (DFT)
40-80 mils (1000-2000 microns)
ASTM D7091
Surface Preparation
NACE 2 / SSPC-SP10 (Near-White Metal Blast)
SSPC-SP10
Adhesion Strength
>1000 psi
ASTM D4541
Elongation at Break
>200%
ASTM D412
Potable Water Approval
NSF/ANSI 61 (if applicable)
NSF/ANSI 61
The Thermodynamics of Galvanic Corrosion in Cooling Tower Basins
Galvanized steel cooling tower basins are inherently susceptible to galvanic corrosion, particularly in the cold-water basin where dissolved oxygen and mineral concentrations are highest. The zinc coating on the steel acts as a sacrificial anode, protecting the underlying steel. However, once the zinc is depleted, often accelerated by aggressive water treatment chemicals, high conductivity, or localized pitting, the exposed steel rapidly corrodes. This degradation is exacerbated by the continuous wetting and drying cycles, thermal expansion and contraction, and abrasive suspended solids present in Southern California's hard water, leading to breaches and costly leaks.
The localized attack often concentrates at seams, bolt connections, and areas of stagnant water or sediment accumulation, creating preferential pathways for corrosion. Traditional patch repairs offer only temporary solutions, failing to address the systemic degradation of the basin's protective layer. Our approach with a flexible elastomeric/epoxy lining creates an impermeable barrier, isolating the compromised galvanized surface from the corrosive water environment. This restores structural integrity and prevents further electrochemical reactions, effectively resetting the corrosion clock for the basin's operational lifespan.
Advanced Surface Preparation and Elastomeric Coating Application
Successful basin coating hinges on meticulous surface preparation. Our UA Local 250 journeymen utilize abrasive blasting to achieve a NACE 2 / SSPC-SP10 near-white metal finish, removing all rust, scale, and spent zinc. This critical step creates an optimal profile (typically 2-4 mils) for mechanical adhesion of the new coating system. Without proper surface profiling, even the most advanced coatings will delaminate prematurely. Following blasting, all seams, corners, and penetrations receive reinforcement with fiber-reinforced epoxies to bridge existing hairline cracks and provide additional structural support, mitigating future stress-induced failures.
The application of a 40-80 mil thick flexible elastomeric/epoxy lining provides a robust, monolithic barrier. These coatings are engineered to accommodate the thermal cycling and minor structural movements inherent in cooling tower operation without cracking or delaminating. The specified thickness ensures long-term abrasion resistance and chemical inertness against common water treatment biocides and scale inhibitors. This comprehensive system, applied by Western Mechanical, Inc., extends the useful life of a corroded basin by 15 years or more, offering a cost-effective alternative to a full tower replacement, which can easily exceed $250,000 for crane, rigging, and new equipment costs.
Lifecycle ROI and Southern California Compliance
Investing in a high-performance basin coating provides significant lifecycle ROI for Southern California facilities. Beyond avoiding the substantial capital expenditure and operational downtime associated with cooling tower replacement, the restored basin integrity reduces water loss from leaks, optimizes water treatment chemical consumption, and improves overall system efficiency. A well-maintained basin prevents biological fouling and corrosion product accumulation, which can impede heat transfer and increase energy consumption. Our solutions are designed to meet stringent local environmental regulations, ensuring compliance and minimizing discharge risks.
Western Mechanical, Inc. understands the unique challenges of operating industrial cooling towers in the arid Southern California climate, where water conservation and operational reliability are paramount. Our coating solutions are tailored to withstand the region's aggressive water chemistries and high ambient temperatures. By extending the life of existing assets, we enable facility managers to defer major capital projects, reallocate budgets, and maintain critical cooling infrastructure with minimal disruption. This proactive maintenance strategy is a cornerstone of sustainable facility management.
UA Local 250 Certified Field Diagnostic & Commissioning Protocol
Verify surface cleanliness to NACE 2 / SSPC-SP10 using visual comparators post-abrasive blasting.
Measure surface profile (anchor pattern) with a digital depth micrometer (e.g., Testex tape) to ensure 2-4 mil profile.
Confirm ambient temperature, surface temperature, and relative humidity are within coating manufacturer's specified ranges using a psychrometer.
Utilize a wet film thickness (WFT) gauge during application and a dry film thickness (DFT) gauge (e.g., magnetic induction) to ensure 40-80 mil coating thickness.
Perform adhesion pull-off test (ASTM D4541) on cured coating to confirm bond strength exceeds 1000 psi.
Facility Director & Chief Engineer FAQs
What types of cooling tower basins can be coated?
Western Mechanical, Inc. specializes in recoating corroded galvanized steel cold-water basins from major OEMs like BAC, Marley, and Evapco. Our process is ideal for basins experiencing pitting, seam leaks, or general surface degradation, extending their operational life significantly.
How long does the coating process typically take?
The duration depends on basin size and condition, but typically, a thorough basin coating project, including abrasive blasting, seam reinforcement, and multi-coat application, can take 3-7 days. We coordinate closely to minimize your facility's downtime.
What is the expected lifespan of a coated basin?
With proper surface preparation and application of 40-80 mil flexible elastomeric/epoxy coatings, facilities can expect an extended lifespan of 15 years or more. This significantly defers the need for costly full cooling tower replacement.
Is this coating process suitable for all levels of corrosion?
Our advanced coating system is highly effective for basins with moderate to severe corrosion, including localized pitting and minor perforations that can be addressed with seam reinforcement. Basins with extensive structural damage may require a more comprehensive assessment.
Acton Headquarters & 24/7 Southern California Dispatch
Western Mechanical, Inc. • 2210 Soledad Canyon Road, Suite O, Acton, CA 93510 • Primary Phone: (661) 251-0111 • 24/7 Toll-Free: (800) 585-5085 • CSLB #618138 (C-20, C-38, C-4)